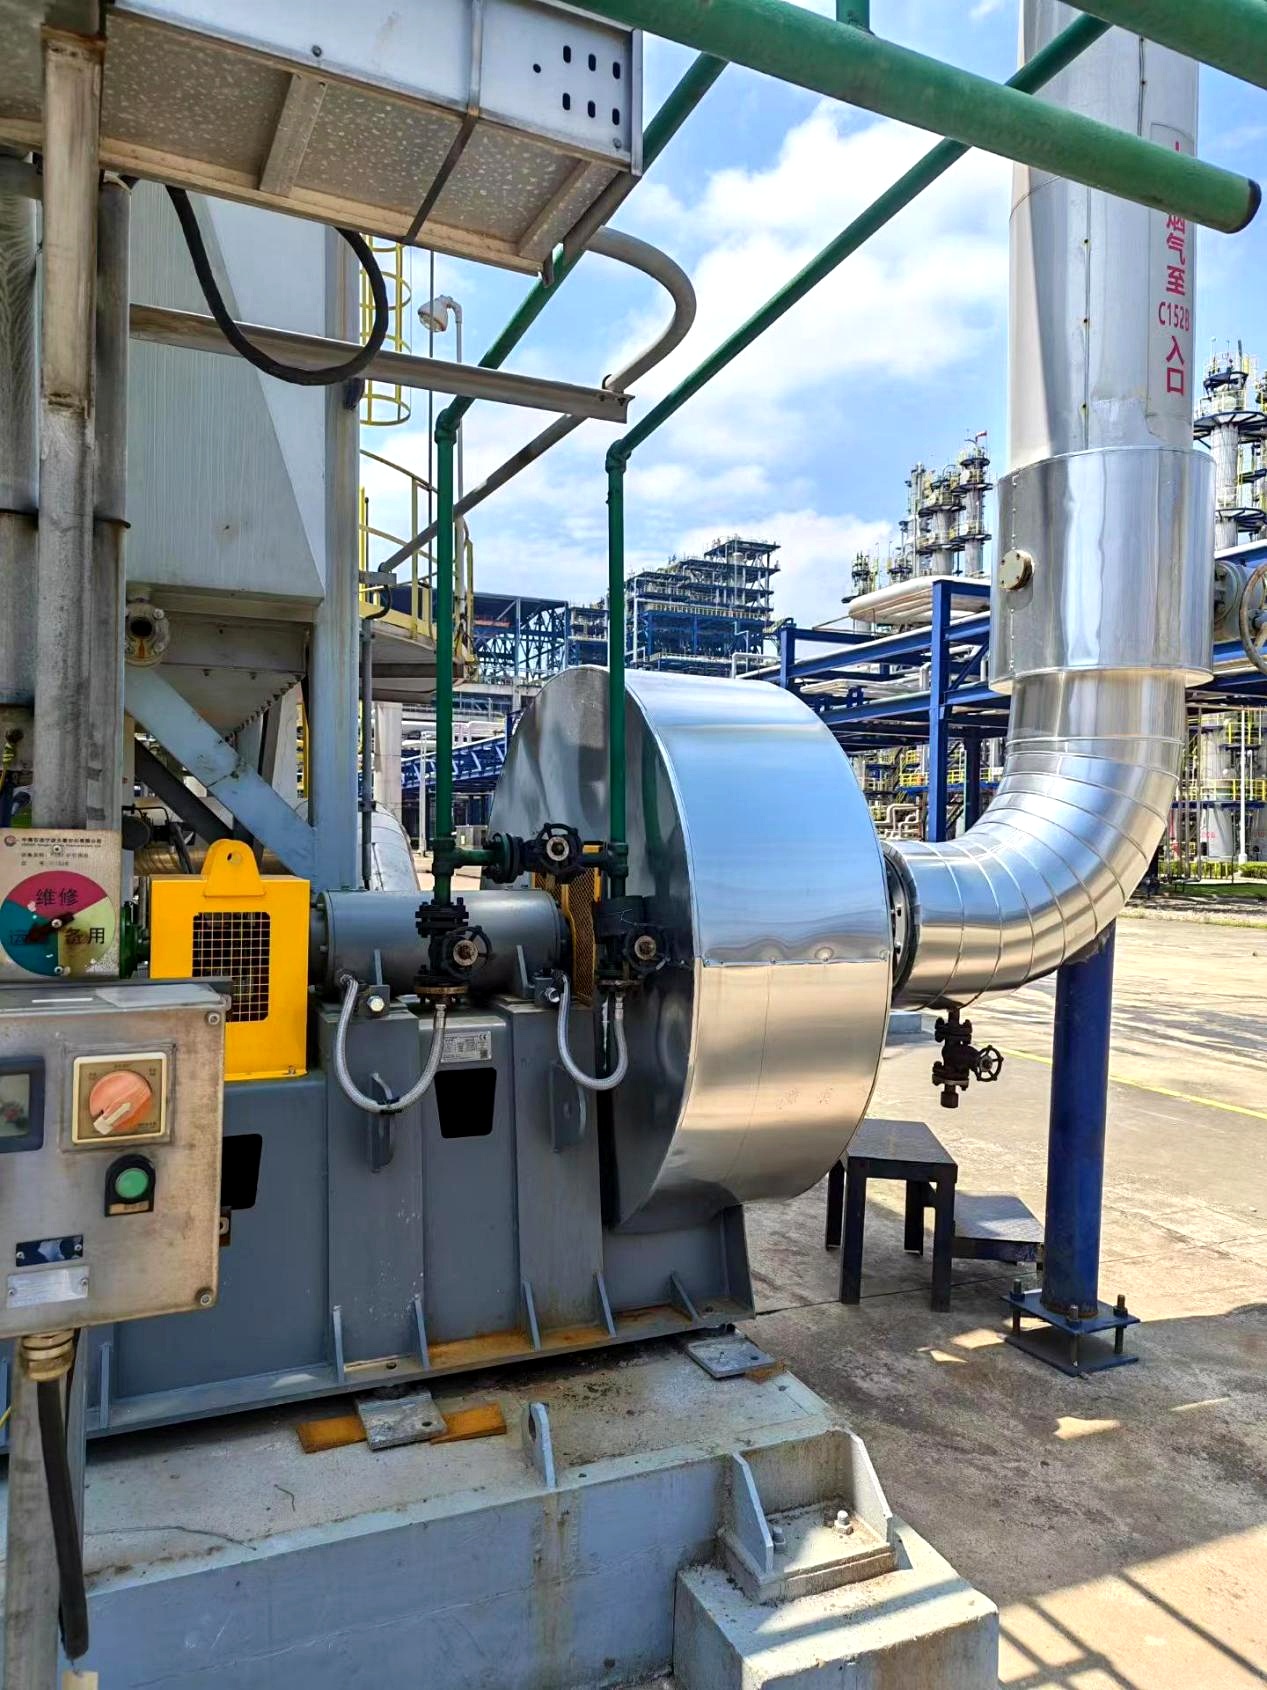
In modern petrochemical and petroleum refining facilities, hydrogen-rich tail gas is often generated as an industrial byproduct. While possessing high calorific potential, this gas stream exhibits intense combustion speeds, elevated flame temperatures, and wide flammability limits. When combined with preheated combustion air exceeding 220°C, conventional burner systems face severe operational hazards, including premature flashback, combustion instability, and high thermal NOx formation.
To address these technical bottlenecks, Eacoon Group was commissioned to deliver an end-to-end combustion system retrofit. The engineering objective was clear: stably burn process byproduct tail gas containing up to 40% hydrogen, operate under continuous high-temperature preheated air conditions, and ensure flue gas NOx emissions remain strictly below 40 mg/m³ across normal operating loads.
To safely handle high hydrogen concentrations and high preheated air temperatures simultaneously, Eacoon implemented a series of patented combustion control architectures:
Hydrogen gas features a laminar burning velocity approximately five to seven times faster than natural gas. Eacoon's proprietary burner design divides the fuel gas feed into central and circumferential staging zones. By introducing fuel in controlled stoichiometric stages, peak localized flame temperatures are suppressed, fundamentally curtailing the thermal (Zeldovich) NOx formation mechanism.
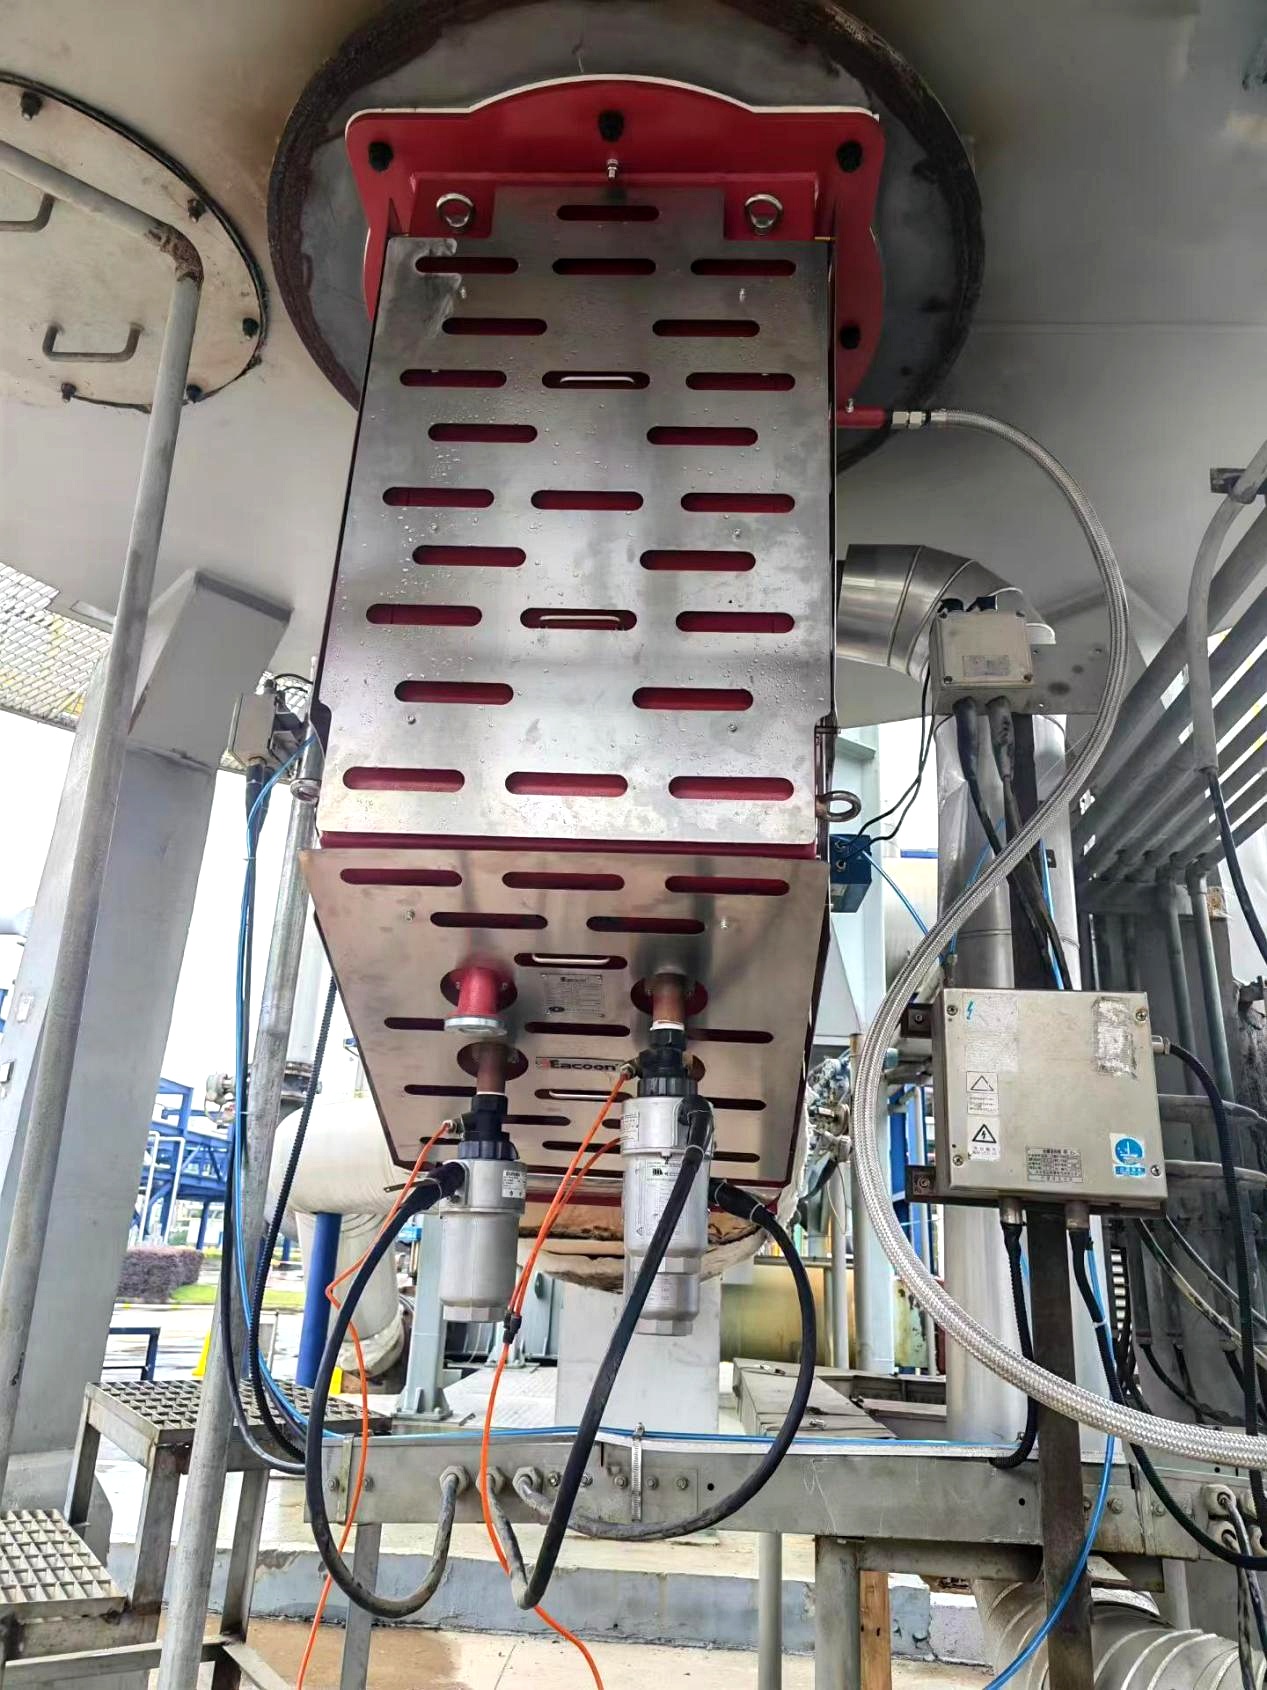
High air preheat (>220°C) demands superior thermal stress resilience and expansion accommodation. As shown in the field equipment inspection below, the burner head is precision-fabricated from high-grade stainless steel with specialized cooling air channels, robust dual ignition probes, and continuous optical flame monitoring sensors to safeguard 24/7 continuous refinery operations.
Following comprehensive on-site commissioning, official flue gas emissions were measured using a calibrated, professional Testo 330LL-2 industrial flue gas analyzer (Serial Number: 03582613). All operational data confirmed stable, compliant performance under actual refinery production loads: Figure 3: On-site Testo 330LL-2 flue gas measurement screen verifying compliance.
| Commissioning Parameter | Measured Field Value | Compliance Target / Benchmark | Engineering Evaluation |
|---|---|---|---|
| Nitrogen Oxides (NOx) | 33.1 mg/m³ (14.8 ppm NO) | Strictly controlled < 40 mg/m³ | Passed with significant compliance safety margin |
| Carbon Monoxide (CO) | 1 ppm (1 mg/m³) | < 100 ppm threshold | Near-zero unburned emissions; complete combustion |
| Flue Gas Oxygen (O₂) | 3.9% | 3.0% – 4.5% target window | Optimized air-to-fuel ratio minimizing thermal heat loss |
| Gross Thermal Efficiency | 82.9% | > 80% industrial target | Delivers direct energy savings for the refinery utility plant |
| Flue Gas Exhaust Temp | 185.1 °C | Standard operational range | Thermal profile safely above acid dew point (57.6°C) |
| Combustion Air Temperature | > 220 °C | High-temperature preheat | Fully recovers industrial waste heat without flame instability |
| Hydrogen Concentration | Up to 40% H₂ | Byproduct tail gas | Stable burner flame envelope without flashback or pulsation |
Yes. Eacoon's intelligent combustion control system incorporates real-time fuel gas Wobbe Index compensation and dynamic air-fuel ratio modulation, safely accommodating hydrogen content fluctuations from 5% to 40% (and up to 100% with dedicated hydrogen-firing models).
By combining aerodynamic internal flue gas recirculation (IFGR), high-velocity micro-orifice fuel gas staging, and flame temperature peak flattening, the burner keeps thermal NOx formation minimal even with high-temperature combustion air.
This solution is widely applicable to petroleum refineries, chemical plants, coking facilities, metallurgical plants, and any industrial facility generating hydrogen-rich, CO-rich, or low-calorific process tail gases.
Connect with Eacoon's senior combustion engineering specialists to evaluate your plant's fuel gas composition, calculate efficiency gains, and design customized ultra-low NOx solutions.
Visit Eacoon Official Website